Shell & Tube Heat Exchanger
Shell & Tube Heat Exchanger
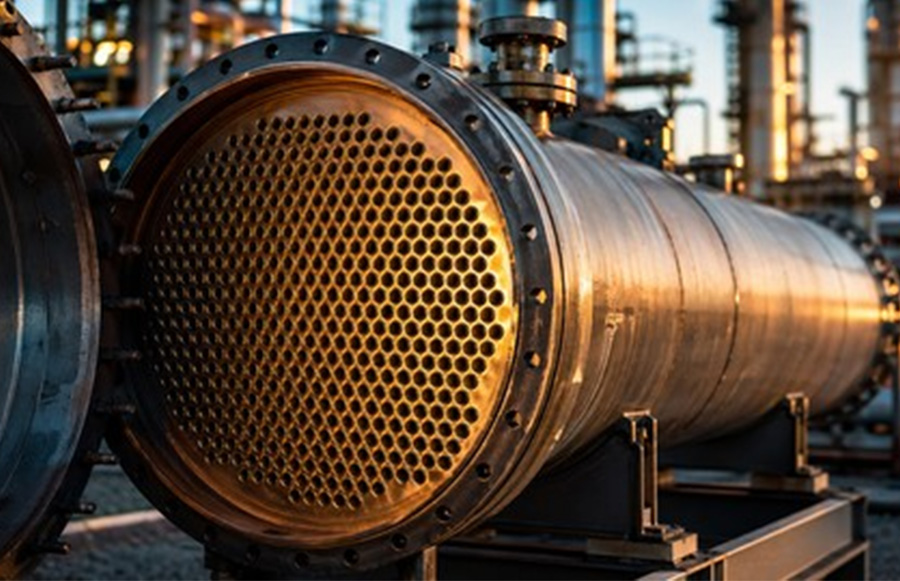
Shell & Tube Heat Exchangers are robust thermal equipment designed for efficient heat transfer between fluids in industrial processes. Their proven construction makes them suitable for heating, cooling, heat recovery, and temperature control applications across various industries.
Degree Kelvin Solutions provides technically suitable Shell & Tube Heat Exchanger solutions based on process conditions, operating temperatures, pressure requirements, flow rates, and application needs. These systems are suitable for process industries, utilities, OEMs, EPC projects, and plant maintenance applications.
Key Features
- Robust Construction – Designed for reliable performance in demanding industrial environments.
- Efficient Heat Transfer – Provides effective thermal transfer between process fluids.
- Flexible Design – Can be configured according to process, temperature, pressure, and flow requirements.
- Wide Application Range – Suitable for heating, cooling, condensation, and heat recovery applications.
- Easy Maintenance – Allows convenient inspection, cleaning, and servicing of heat transfer surfaces.
- Reliable Operation – Supports consistent heat transfer performance for continuous industrial processes.
Applications
- Process Heating – Used for heating process fluids to required operating temperatures.
- Process Cooling – Provides controlled cooling for industrial fluids and processes.
- Oil Cooling – Suitable for cooling lubricating, hydraulic, and process oils.
- Condensation – Used for condensing vapors and recovering useful process heat.
- Heat Recovery – Helps recover thermal energy from hot process streams.
- Chemical Industries – Supports heating and cooling requirements in chemical processes.
- Food & Beverage – Used for controlled heating and cooling in processing applications.
- Industrial Utilities – Suitable for hot water, chilled water, steam, and other utility systems.